|
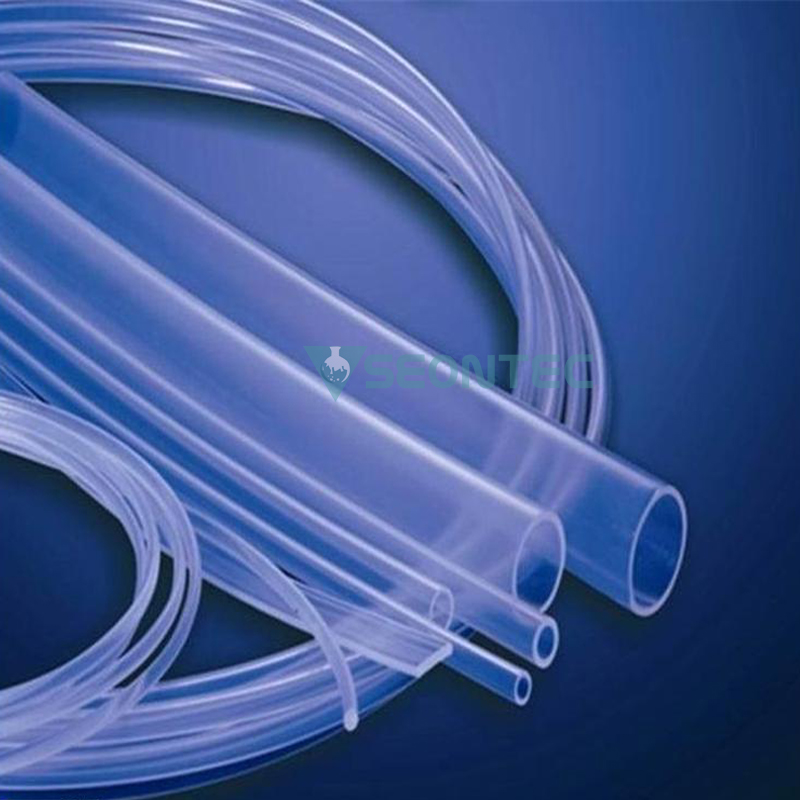
High-Performance PFA Hoses: The "Golden Pipeline" for Semiconductors and High-End ManufacturingIn high-end fields such as semiconductor manufacturing and biopharmaceuticals, a small hose carries the crucial mission of maintaining process purity—this is the PFA hose, an indispensable core component due to its superior chemical stability and high purity. PFA (perfluoroalkoxyalkane) hoses are high-performance fluoroplastic tubing with excellent chemical inertness, high purity, and temperature resistance. They excel in conveying ultrapure chemicals and corrosive media, becoming the "vascular system" of high-end manufacturing industries such as semiconductors, pharmaceuticals, and chemicals. Core Characteristics of PFA Hoses PFA hoses are copolymerized from tetrafluoroethylene and perfluoroalkyl vinyl ethers. Their unique perfluorinated molecular structure endows them with multiple superior properties. Chemical Resistance: Resistant to strong acids, strong alkalis, and organic solvents, including most corrosive chemicals such as concentrated sulfuric acid and hydrofluoric acid. High Purity: Ultra-low leaching characteristics; metal ion content can be controlled at the ppb (parts per billion) level, meeting semiconductor-grade purity requirements. Temperature Resistance: Wide operating temperature range (-80°C to +260°C), adaptable to various environments from ultra-low temperature cooling to high-temperature sterilization. Physical Properties: Mirror-smooth inner wall, low fluid resistance; good flexibility, easy installation,anti-aging, long service life. Wide Range of Applications: Semiconductor Manufacturing: In chip production, PFA tubing is used to transport ultrapure chemicals, high-purity water, and specialty gases, ensuring that nanoscale circuits are not contaminated. Biopharmaceuticals: As tubing in bioreactors, culture medium delivery, and purification systems, it meets cGMP cleanliness requirements, ensuring drug safety. Chemical Industry: Essential for transporting various corrosive chemical reagents, especially in the production of high-purity chemicals. New Energy Field: Widely used in emerging fields such as lithium-ion battery electrolyte preparation and fuel cell systems. Specialty PFA Tubing Meets Diverse Needs To meet the specific needs of different industries, several specialty PFA tubing categories have been developed. Semiconductor Grade PFA Tubing: Highest purity, metal ion deposition below 0.1 ppb, conforming to SEMI F57 standards. Conductive PFA tubing: Contains conductive materials to prevent static electricity buildup, suitable for flammable and explosive environments. Reinforced PFA tubing: Features braided reinforcement for improved pressure resistance, suitable for high-pressure delivery systems. Transparent PFA tubing: Maintains excellent chemical stability while offering good transparency for easy observation of fluid conditions. Broad Market Prospects According to industry reports, the global PFA tubing market reached $850 million in 2023 and is projected to grow to $1.23 billion by 2028, representing a CAGR of approximately 7.5%.
This growth is primarily driven by the expansion of the semiconductor industry, the development of the biopharmaceutical industry, and increased demand in the new energy sector. The Asia-Pacific region, particularly China, will be the fastest-growing market.
With the accelerated localization of China's semiconductor industry and the continuous upgrading of high-end manufacturing, the high-performance PFA tubing segment is experiencing unprecedented development opportunities, becoming one of the key materials supporting "Made in China 2025".
|